
درباره سایت
آخرین مطالب
- Review of the Application of Limonite Oxide (Gol Mash) in Various Industries
- دراسة تطبيق أكسيد الليمونيت (غول ماش) في مختلف الصناعات
- بررسی کاربرد اکسید لیمونیت (گل ماش) در صنایع مختلف
- کائولن باکیفیت کانی سنگ امیران برای کاغذ و رنگ مش 450 تا 1500
- استعلام قیمت فلدسپات صنایع لعابسازی از وبسایت کانی سنگ
- تالک صنعتی و کاتالوگ فنی برای صنایع رنگ و لاستیک
- کربنات کلسیم ۲۰۰۰ مش با ذرات کنترلشده برای پروفیل UPVC
- فلدسپات مناسب کانی سنگ با دانهبندی یکنواخت کاشی درجه
- کربنات کلسیم ۱۲۵۰ مش با ترکیب شفاف برای کابل صنعتی
- تالک صنعتی مناسب صنایع پلیمر با دانه بندی دقیق و کنترل شده
امکانات وب
Introduction to Coated Calcium Carbonate and Its Role in Maintaining Transparency and Color Quality
In today's polymer industry, compound and base polymer granules are the foundation of thousands of industrial and household products, and competition in this market relies more on the "visual quality" of products than on price. Clean color, uniform surface, and desirable transparency are the first criteria a professional buyer examines in a polymer part. Among these, coated calcium carbonate, as one of the most widely used mineral additives, plays a very decisive role in maintaining these characteristics.
Coated calcium carbonate is a form of calcium carbonate in which the particle surfaces are coated with a thin organic coating layer, usually based on fatty acids. This coating is not just a simple protective layer; it acts as an interface between a polar mineral particle and a non-polar polymer matrix. Without this interface, mineral particles tend to agglomerate, absorb moisture, and disperse poorly—and it is precisely these events that reduce the product's transparency and make its color dull and cloudy.
In fact, when a manufacturer uses coated calcium carbonate in the formulation of compounds, polymer granules, profiles, cables, flooring, or PVC parts, they are not merely looking to make the formula cheaper. They are using an additive that can maintain the transparency and color quality of the final product at a high level while reducing costs. This is why choosing the right mesh and the appropriate coating type is a technical decision, not just a purchasing one.
The mesh range of 450 to 3500 for this product demonstrates the breadth of its applications. On one hand, we use it in parts requiring an economical filler with relative transparency, and on the other hand, in finer compounds and granules where transparency and color quality are paramount, a higher mesh offers better performance. In the rest of the article, we will examine how this material maintains such characteristics and what factors play a role in this process.
In the upcoming chapters, we will first examine the coating structure and its importance, then discuss the relationship between particle size (mesh) and transparency, and afterward, delve into the applications of coated calcium carbonate in compounds, granules, profiles, cables, flooring, and PVC parts, and finally, present the criteria for selecting the appropriate mesh to maintain transparency and color.
Coating Structure; Why is Surface Coating So Important for Transparency?
To understand why coated calcium carbonate maintains transparency, we must look at the particle surface. Calcium carbonate particles in their natural state, i.e., the uncoated type, have a polar and hydrophilic surface. This surface has a strong tendency to absorb moisture and stick together. When such particles enter a non-polar polymer matrix like polypropylene, polyethylene, or PVC, they do not bond with the matrix and remain together as agglomerates.
Physically, these agglomerates are small wells of defect in the product's structure. When light shines on the product surface, it scatters intensely at the boundaries of these agglomerates, resulting in reduced transparency and a cloudy, opaque color. But when the particle surface is coated with an organic layer, the surface energy decreases, the particles do not absorb moisture, and instead of sticking together, they are distributed as separate, dispersed particles within the polymer matrix.
The surface coating also allows the particles to form a better bond with the polymer matrix. This better bond means higher packing density, fewer voids, and consequently, less disruption to the light path. This is why using the coated type is almost mandatory in products where transparency and color are critical. Manufacturers who use the uncoated type usually face a severe drop in transparency, dull color phenomena, and even gas evolution during production.
Interestingly, coating helps maintain color quality in addition to transparency. Uncoated particles can act as weak catalysts, accelerating the thermal degradation of the polymer during the curing or extrusion process, which results in the product yellowing. The surface coating largely limits this direct contact between the mineral particle and the polymer chain, helping the product's color stability during production and even throughout its service life.
Ultimately, surface coating means improved processability. Lower friction between particles, less heat in the extruder, less adhesion to walls, and less equipment wear are all benefits of coating. These characteristics indirectly help maintain transparency and color quality, because a more stable production process entails less quality loss. For this reason, coated calcium carbonate is not just a filler, but a "process facilitator."
Particle Size and Mesh; The Direct Relationship Between Mesh and Product Transparency
One of the most important factors in the performance of coated calcium carbonate is its particle size, which is specified in the industry by the term "Mesh". The 450 to 3500 mesh range shows that this product is available in a wide spectrum of particle sizes. As the mesh number increases, particles become finer and the particle size distribution is better controlled. This has a direct impact on the transparency of the final product.
The relationship between particle size and transparency is a physical one based on the interaction of light and particles. When light passes through a material, it scatters and refracts at the boundary of any particle whose size is comparable to the wavelength of light. Larger particles create more scattering, meaning reduced transparency and increased haze. In contrast, very fine particles—so small they are below the wavelength of visible light—create less scattering, and the product's transparency is better preserved.
This is why in applications where transparency and color quality are priorities, higher meshes such as 1500 to 3500 are typically used. These fine particles, along with the appropriate coating, can produce final products with high transparency and very clean color. On the other hand, in thicker polymer parts, profiles, and flooring that require more mechanical strength and less transparency, 450 to 1200 mesh is a more logical choice.
In addition to average particle size, "particle size distribution" is also very important. If fine and coarse particles coexist in a sample, the coarse particles create intense scattering points that lower the product's transparency. A high-quality coated calcium carbonate, besides having an appropriate average mesh, has a narrow particle size distribution, meaning consistent performance throughout the product.
Another point is that selecting the appropriate mesh should be tailored to the polymer type and production process. A 3500 mesh might work excellently in a polypropylene base, but in a rigid PVC formulation, maybe a 1200 mesh is the best choice considering other additives. Ultimately, choosing the right mesh is a multidimensional decision that must be made based on the polymer type, product thickness, process conditions, and of course, the expected level of transparency and color quality.
Application of Coated Calcium Carbonate in Compound and Polymer Granules
Compound and polymer granules are the base forms of polymeric materials used in a wide range of industries. In these products, coated calcium carbonate plays a dual role: on one hand, an economical filler to reduce the final price, and on the other, an agent to control physical and visual properties. This is why choosing its type and mesh is considered a strategic decision in compounding plants.
In compound production, the first challenge is the uniform dispersion of calcium carbonate in the polymer matrix. Coated particles have lower surface energy due to their organic coating and disperse better and faster in the polymer matrix. This good dispersion means preventing particle agglomeration and thus maintaining transparency and color uniformity in the final granule. In fact, the quality of dispersion in the compound directly transfers to the visual quality of the final product.
One of the most important issues in compound and granule production is color stability during production. At high extrusion temperatures, polymers are prone to degradation and yellowing. The surface coating of coated calcium carbonate, by reducing direct contact between the mineral particle and the polymer chain, reduces thermal degradation and helps the product's color stability. To read more on this topic, you can study the article How Does Coated Calcium Carbonate Help Polymer Thermal Stability?
In polymer granule production, granule transparency is often an important quality indicator, even if the final product is not transparent. Dull and colorless granules usually indicate problems in the process or raw material quality. Coated calcium carbonate with a high mesh (such as 2500 to 3500), can help produce granules with excellent transparency and perfectly clean color, which ultimately transform into a higher-quality final product.
Ultimately, using coated calcium carbonate in compounds also means reducing other costs. Due to better dispersion, less energy is required for mixing, and production speed increases. Also, less equipment wear due to the surface coating reduces maintenance costs. All these factors place the compound made with this material in a favorable position economically and qualitatively.
Applications in Profiles, Cables, Flooring, and PVC Parts
In addition to compounds and granules, coated calcium carbonate has widespread applications in final products such as profiles, cables, flooring, and PVC parts. In these products, besides transparency and color quality, other issues such as mechanical strength, durability against environmental conditions, and product lifespan are also important. The surface coating of this material helps both aspects.
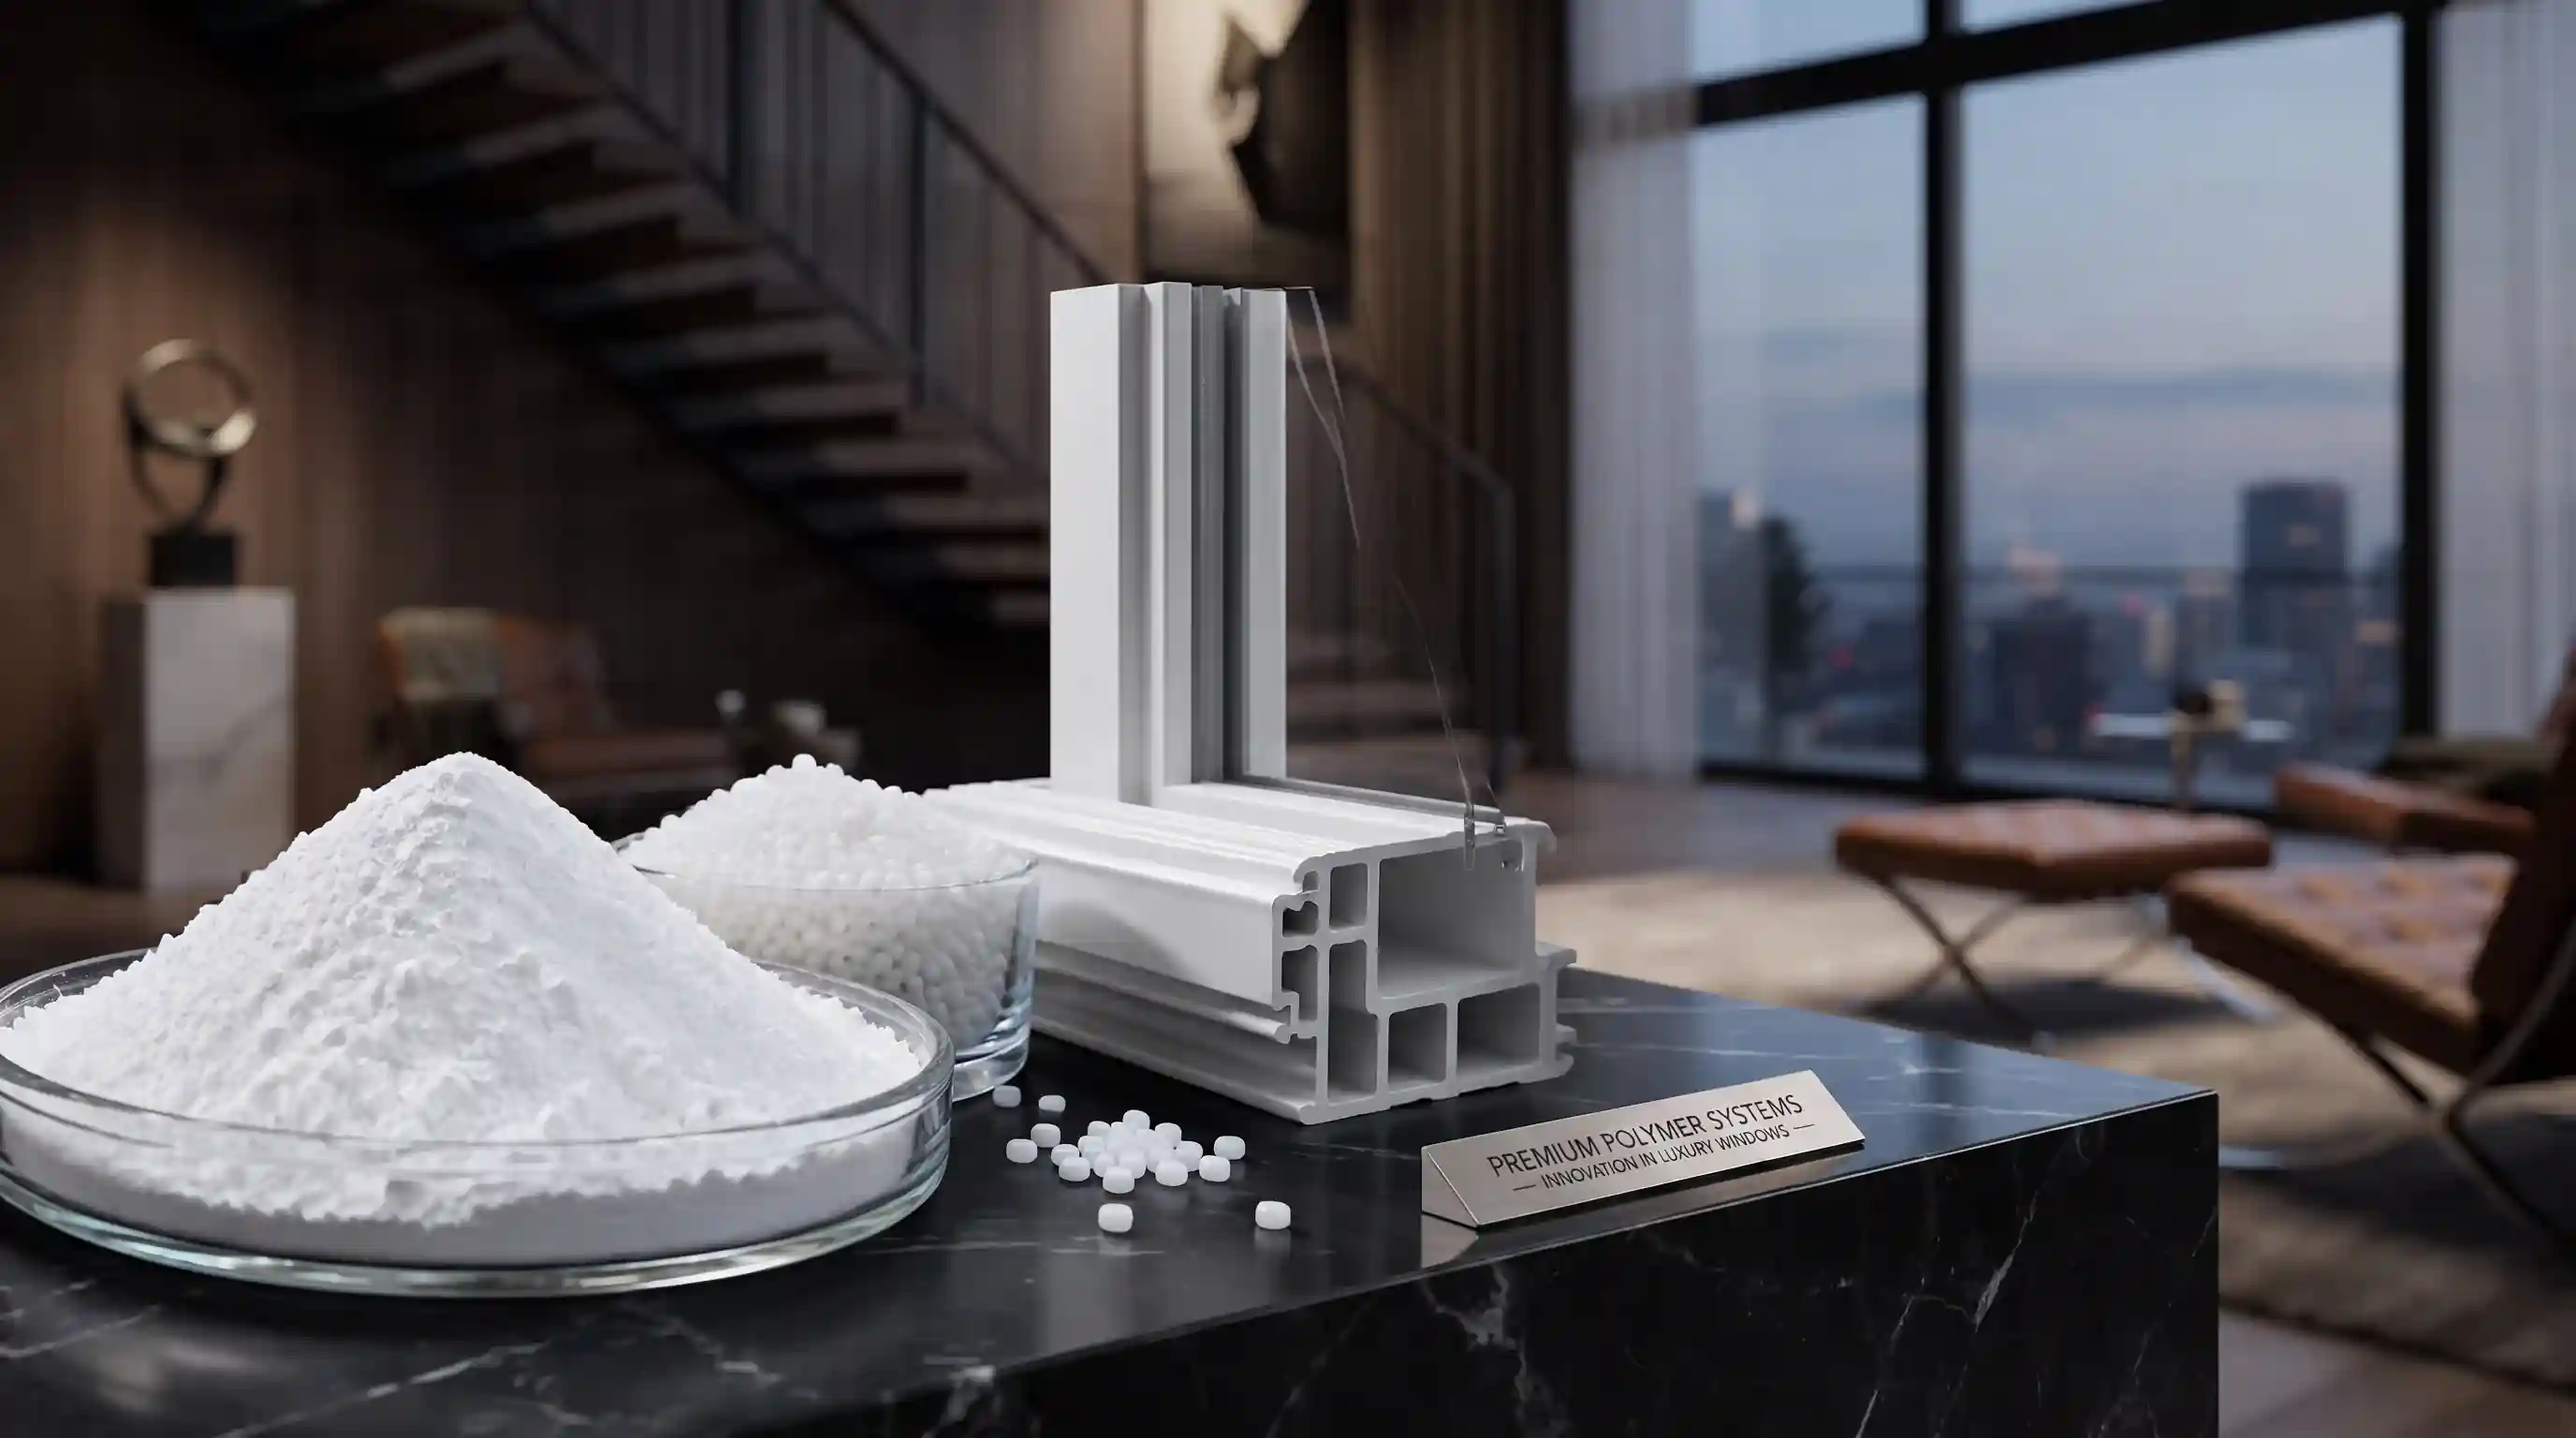
In the production of UPVC profiles, often used for windows and doors, a bright and uniform white color is one of the most important quality indicators from the customer's perspective. Using coated calcium carbonate with an appropriate mesh not only helps maintain a clean white color but also prevents the profile from yellowing over time and when exposed to sunlight. Also, good particle dispersion gives the profile a smooth and flawless surface, which is very important in installation and use.
In the cable industry, coated calcium carbonate is used as a filler in polymer sheaths and insulations. Here, besides electrical and mechanical properties, the appearance of the cable sheath matters, especially in colored cables. Uniform color dispersion and the absence of dull spots or stains add to the overall quality of the cable and perform better in quality control tests. Interestingly, for greater resistance of polymer products, choosing the right mesh and coating plays an important role; on this topic, you can read the article How Does Coated Calcium Carbonate Increase the Resistance of Polymer Products?
In PVC floorings and polymer parquets, transparency and color quality are directly related to the product's aesthetics. Floorings made from coated calcium carbonate with a high mesh and appropriate coating have brighter colors, a glossier surface, and better wear resistance. Also, in rigid PVC parts such as pipe fittings, pipes, and accessories, this material helps maintain the classic white color and prevents discoloration over time.
In all these applications, a common principle exists: the visual quality of the product is directly related to the quality of raw materials and the production process. Using appropriate coated calcium carbonate, with a mesh suited to each application, is one of the most effective ways to achieve products with stable transparency and color. This choice leads to final customer satisfaction and reduces quality loss and production waste.
Color Quality Maintenance Mechanism; From Light Scattering to Preventing Yellowing
Color quality in polymer products is influenced by two groups of factors: physical factors such as light scattering, and chemical factors such as thermal and photo-degradation. Coated calcium carbonate responds effectively to both groups, making it a key additive for maintaining color quality.
Physically, the color quality of a polymer product depends on the amount of light scattering on its surface and within its depth. When particles are distributed uniformly and with appropriate size in the polymer matrix, light is reflected regularly, and the product's color appears transparent and vibrant. In contrast, the presence of agglomerates or coarse particles creates irregular light scattering, making the product's color dull, grayish, or two-toned. The surface coating of coated calcium carbonate minimizes this irregular scattering by preventing agglomeration.
Chemically, one of the most important challenges in polymer products is yellowing. This phenomenon, which occurs due to thermal, photo, or oxidative degradation of the polymer, can rapidly degrade the product's appearance. Uncoated mineral particles can intensify this process by accelerating thermal degradation. But the surface coating of coated calcium carbonate acts as an insulation layer, reducing direct contact between the particle surface and the polymer chain. This improves the product's thermal and color stability.
In addition, in colored products, coated calcium carbonate acts as a transparent substrate where pigments disperse well. This characteristic is especially important in paint making and colored masterbatch production. To read more about this topic, we recommend the article Comprehensive Guide to Using Coated Calcium Carbonate in Paint Making.
Another notable point is the effect of moisture on color quality. Uncoated particles absorb moisture, and during the process, this moisture tus into steam, which can create voids and spots on the product surface. These voids not only reduce transparency but also make the product's color inconsistent and of poor quality. Coated calcium carbonate minimizes this problem due to its hydrophobic coating, helping to maintain the integrity of the product's color and surface.
Quality Control and Selecting the Appropriate Mesh to Maintain Transparency
Choosing the right coated calcium carbonate to maintain transparency and color quality is a multi-step process that requires a precise understanding of the product, the process, and final requirements. In this section, we examine the key criteria for this choice.
1. Mesh selection based on application: As mentioned, the 450 to 3500 mesh range allows for a wide selection. For compounds and granules where transparency is critical, 2500 to 3500 mesh is recommended. For profiles and flooring, 1000 to 2000 mesh performs well, while for thick PVC parts and cables, 450 to 1200 mesh is usually sufficient. Mesh selection should be done based on product thickness, polymer type, and process conditions.
2. Coating quality: The quality of the surface coating is as important as particle size. A good coating should be uniform, complete, and present in the right amount. Over-coating can lead to problems like tackiness and reduced process efficiency, while insufficient coating eliminates the benefits of the coated type. Reputable manufacturers usually provide comprehensive information about the type and amount of coating.
3. Production uniformity and stability: Consistency in production is one of the most important criteria in selecting a supplier. Changes in particle size or coating quality from one production batch to another can cause severe fluctuations in the product's transparency and color. Strict quality control—including particle size distribution tests, coating amount, moisture, and color—guarantees that every batch of the product performs identically.
4. Particle size distribution: In addition to average particle size, their distribution also matters. A product with a narrow distribution offers better transparency because there are no very coarse particles that cause severe light scattering. Requesting precise particle size distribution information from the supplier is a smart move.
Ultimately, choosing the right coated calcium carbonate is an investment in quality. Saving on purchase costs by selecting an inappropriate product can lead to quality loss, increased waste, and customer dissatisfaction. Therefore, a proper balance must always be struck between price and performance.
Conclusion: Why is Coated Calcium Carbonate a Smart Choice?
In this article, we examined how coated calcium carbonate maintains the transparency and color quality of polymer products. From the surface coating structure and its role in preventing particle agglomeration, to the importance of particle size and mesh, and from the broad applications in compounds, granules, profiles, cables, flooring, and PVC parts, to the physical and chemical mechanisms of maintaining color and transparency.
Our most important takeaway from this review is that transparency and color quality are not simply the output of one production stage, but the result of a set of smart decisions in raw material selection and process setting. Choosing a coated calcium carbonate with high-quality coating and a mesh appropriate to the application is one of the most impactful of these decisions. This choice not only enhances the product's visual quality but also helps production process stability, waste reduction, and ultimately, final customer satisfaction.
Another advantage of this material is its high diversity. The 450 to 3500 mesh range means there is a suitable product for any type of application, from delicate compounds to resistant floorings. This flexibility allows manufacturers to fine-tune their formulations and find the best balance between price and quality. Also, side benefits such as reduced equipment wear, lower energy consumption, and improved production speed double the value of this material.
Finally, if you are also active in the compound, granule, or polymer parts industry and are looking for a product that keeps the transparency and color quality of your products at a high level, we suggest you check out the Coated Calcium Carbonate product from Kani Sang Amiran Project. By choosing the right mesh and appropriate coating quality, you can see the real difference in your final products.
We hope this article has helped you better understand this material and choose the most suitable option for your needs. If you need further guidance on selecting the right mesh, contact our technical experts.
| Question | Answer |
|---|---|
| What is coated calcium carbonate? | It is calcium carbonate whose particle surfaces are coated with an organic layer (usually based on fatty acids) to ensure better dispersion in the polymer matrix, lower moisture absorption, and maintained transparency and color. |
| Why does coated calcium carbonate maintain product transparency? | The surface coating prevents particle agglomeration and reduces light scattering; as a result, the product will have better transparency and a cleaner color. |
| What is the difference between the coated and uncoated types? | The uncoated type has a polar and hydrophilic surface that causes agglomeration, moisture absorption, and a drop in transparency, while the coated type offers better dispersion in the polymer by reducing surface energy. |
| What is the mesh range of this product? | The mesh range of this product is 450 to 3500 mesh, allowing selection tailored to the type of application. |
| Which mesh is more suitable for maintaining transparency? | Generally, higher meshes (such as 2500 to 3500) create less light scattering due to finer particle sizes and offer better transparency. |
| What are the main applications of this product? | Compound, polymer granules, profiles, cables, flooring, and PVC parts are the main applications of this product. |
| Does this material prevent product yellowing? | The surface coating reduces direct contact between the mineral particle and the polymer chain and helps the product's thermal and color stability, although process conditions must also be controlled. |
| Why is the coated type used in compounds and granules? | Because it provides better dispersion, reduced moisture, color stability at extrusion temperature, and a cleaner surface for the final granule. |
| Should the mesh be selected based on the polymer type? | Yes; polymer type, product thickness, and process conditions all affect selecting the appropriate mesh and maintaining final transparency. |
| Where can I see more product information? | The product page is available on the Kani Sang Amiran Project website, and you can contact our technical experts to select the appropriate mesh. |
The technical specifications, mesh range (450 3500 mesh), and product applications are prepared based on information published on the Kani Sang Amiran Project website.
برچسب: Coated Calcium Carbonate,How Does Coated Calcium Carbonate Maintain Transparency and Color Quality?,
نویسنده: رساوب آفرین